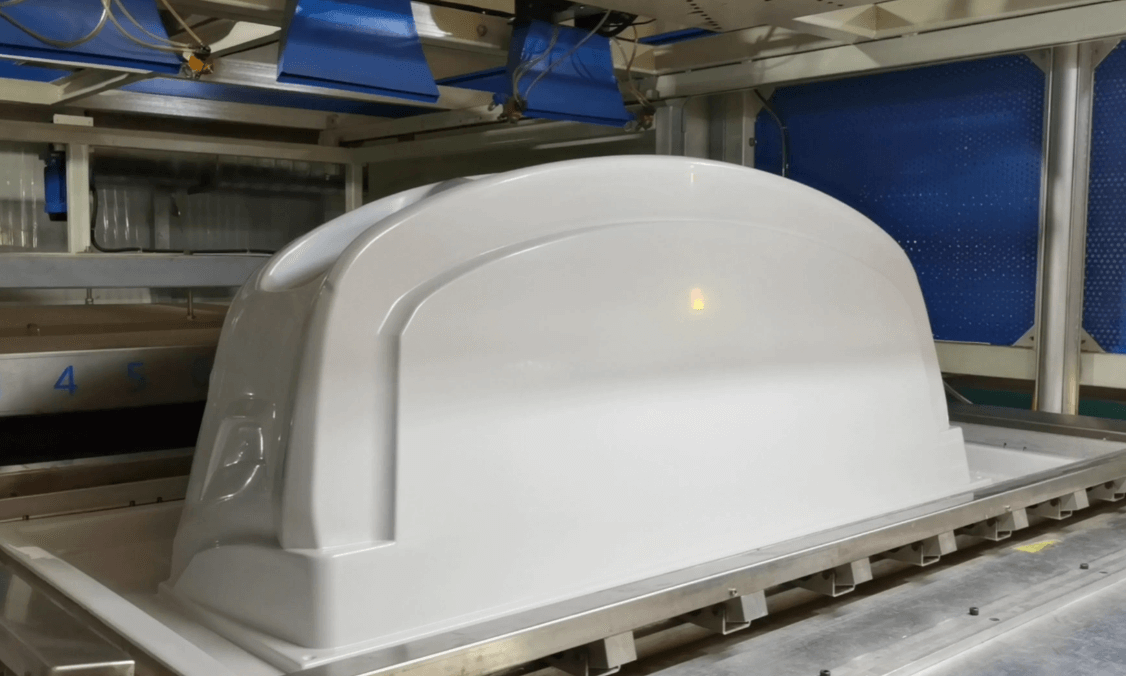
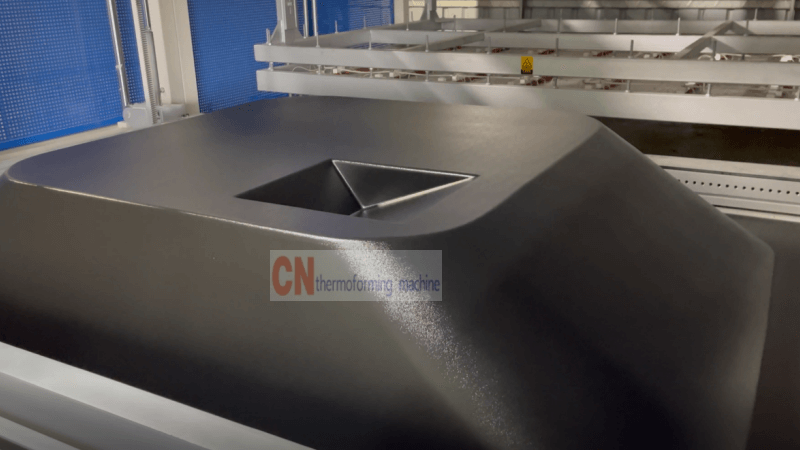
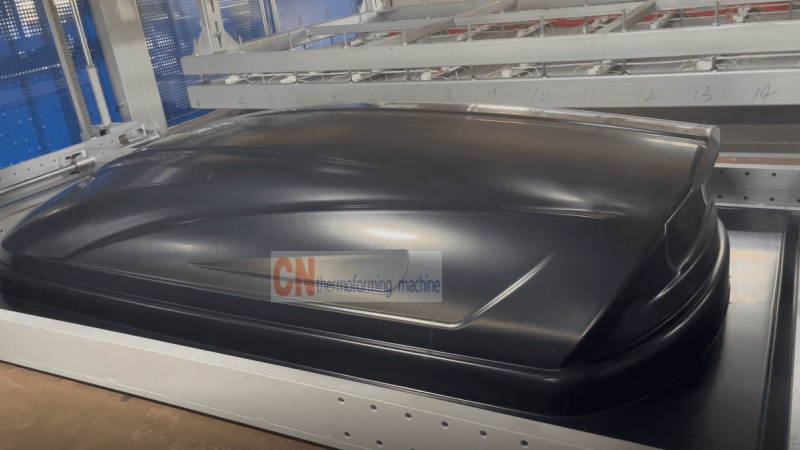
Heavy gauge thermoforming is the process of heating a thermoplastic sheet until it reaches a suitable forming condition and then shaping it over or into a mold.
The sheet is first heated within a controlled temperature range. Once the material reaches the required forming condition, it is transferred to the mold or forming station. Vacuum, air pressure, mechanical movement, or a combination of forming methods is then used to bring the heated sheet into contact with the mold surface.
After forming, the part is cooled while maintaining the required geometry. The formed component can then be trimmed, drilled, machined, or transferred to subsequent assembly operations.
The basic sequence is:
Sheet Preparation → Heating → Temperature Stabilization → Forming → Vacuum / Pressure Application → Cooling → Demolding → Trimming
The process appears straightforward, but thick sheet introduces additional thermal and mechanical variables that must be controlled during development.
The main difference is not simply the thickness of the sheet.
A thicker sheet contains a larger volume of material that must reach a suitable forming condition. Heat therefore needs to travel from the heated surfaces toward the center of the sheet.
This creates a potential temperature gradient:
Heated Surface → Outer Layer → Middle Layer → Core → Opposite Surface
If the outside becomes too hot before the center reaches the required temperature, the sheet may have an unsuitable temperature profile when forming begins.
This can lead to:
For this reason, heavy gauge thermoforming should be treated as a thermal process as well as a forming process.
Heating is one of the most critical stages of the process.
The objective is not simply to make the sheet surface hot. The objective is to establish a temperature profile through the thickness that provides sufficient flexibility and controlled material flow during forming.
Several variables influence heat penetration:
A thick sheet can therefore require a different heating strategy from a thin sheet even when the material is the same.
One of the common process-development challenges is the difference between surface temperature and internal temperature.
For example, a sheet may appear sufficiently hot when measured at the surface while the center remains significantly cooler.
If forming begins too early, the core may resist deformation while the outer layers stretch more easily.
The result can be uneven material distribution and inconsistent forming behavior.
Temperature measurement and process development should therefore consider not only the measured surface temperature but also how heat has penetrated through the sheet.
There is no single forming temperature that applies to every thermoplastic material or every application.
The appropriate forming window depends on:
The objective is to identify a process window in which the sheet can deform sufficiently while still maintaining controlled material distribution.
If the sheet is too cold, it may resist forming and fail to reproduce the mold geometry.
If it is too hot, the material may become excessively soft, resulting in uncontrolled stretching, sagging, thinning, or surface defects.
For production development, the forming temperature should therefore be established through controlled trials rather than relying only on a nominal material temperature.
One of the most important engineering considerations is where the material moves during forming.
The original sheet has a relatively uniform thickness. After forming, however, different regions of the finished part may have different wall thicknesses.
Material tends to move toward areas experiencing greater deformation.
Deep cavities, sharp transitions, corners, and areas with significant stretching can therefore become thinner than relatively flat regions.
A useful way to think about the process is:
Initial Sheet Thickness → Heating → Stretching → Material Redistribution → Final Wall Thickness
The objective is not necessarily to maintain perfectly uniform thickness everywhere.
Instead, the process should produce a wall-thickness distribution that remains suitable for the mechanical and dimensional requirements of the finished part.
Localized thinning is one of the most common concerns in heavy gauge forming.
A part may have sufficient average wall thickness but still contain local areas where the material has become significantly thinner.
These areas can occur around:
The location of maximum thinning depends on the relationship between the original sheet and the mold geometry.
Excessive thinning can affect:
Process development should therefore evaluate wall thickness distribution rather than judging a formed part only from its external appearance.
Where necessary, sheet thickness, heating distribution, mold geometry, forming sequence, and starting-sheet dimensions can be adjusted to improve material distribution.
Forming depth strongly affects how the sheet stretches.
A shallow feature may require relatively little material movement, while a deep cavity can require substantial deformation.
A useful engineering concept is the relationship between the initial sheet dimensions and the final mold geometry.
The deeper and more complex the geometry becomes, the more important it is to evaluate:
Deep forming does not automatically mean that a part cannot be produced.
The important question is whether the sheet can be distributed through the geometry without creating unacceptable thinning or other defects.
Corner geometry has a direct influence on material movement.
Sharp corners force the sheet to change direction over a short distance. During forming, this can concentrate deformation in a relatively small region.
Larger radii generally provide a smoother transition and can allow the material to distribute more gradually.
This is particularly important for:
Corner radius should therefore be considered during mold design rather than treated as a cosmetic detail.
The interaction between radius, forming depth, sheet thickness, and material properties can significantly affect the final wall-thickness distribution.
The mold does more than define the external shape of the product.
Its geometry controls how the heated sheet moves during forming.
Important mold characteristics include:
A well-designed mold helps the heated sheet move progressively into the required geometry.
Poorly considered geometry can create localized stretching, trapped air, incomplete forming, difficult demolding, or excessive dimensional variation.
For complex parts, mold design and process development should therefore be considered together.
See also: Thermoforming Mold Design.
Vacuum is used to remove air between the heated plastic sheet and the mold surface so that atmospheric pressure can push the sheet against the mold.
The basic principle is:
Heated Sheet → Mold Positioning → Air Removal → Sheet-Mold Contact → Cooling
For large or deep parts, vacuum performance becomes increasingly important.
The required vacuum system depends on factors such as:
Vacuum cannot effectively pull the sheet into an area where trapped air cannot escape.
Vent holes and vacuum channels therefore play an important role in forming quality.
Poor venting can result in:
Vent locations should be considered according to the actual geometry and expected material movement.
See also: Thermoforming Vacuum System and Vacuum Forming.
Forming does not end when the sheet reaches the mold.
The part must remain sufficiently stable while cooling.
Thermoplastics contract as they cool, and the amount and direction of shrinkage depend on the material, processing history, geometry, wall thickness, and cooling conditions.
Uneven cooling can therefore produce:
Large and thick parts can be particularly sensitive because different areas may cool at different rates.
The cooling process should therefore be considered as part of the forming cycle rather than as a separate final step.
Possible causes:
Typical result:
Some areas form too easily while others remain relatively stiff.
Process response:
Review the heating profile across the sheet and through its thickness before changing forming parameters.
Possible causes:
Typical result:
A specific area becomes significantly thinner than the surrounding wall.
Process response:
Review material flow, heating distribution, geometry, and starting-sheet size together.
Possible causes:
Typical result:
The sheet does not fully contact the mold in certain areas.
Process response:
Check the complete vacuum path, venting layout, forming temperature, and mold geometry.
Possible causes:
Typical result:
The part changes shape after demolding or during subsequent cooling.
Process response:
Review cooling conditions and dimensional stability rather than correcting the problem only through trimming.
Possible causes:
Typical result:
Parts produced under apparently identical conditions show dimensional differences.
Process response:
Establish a stable process window and monitor the variables that have the greatest influence on part dimensions.
Good thermoformed parts begin with geometry that supports controlled forming.
During product and mold development, several design factors should be evaluated together.
Deep features require greater material movement and should be evaluated for potential localized thinning.
Smooth transitions generally provide better material movement than abrupt geometric changes.
Adequate draft can make demolding easier and reduce the risk of deformation during part removal.
Abrupt changes in geometry can concentrate deformation. Gradual transitions can improve material distribution.
Structural features can improve stiffness, but their geometry must be considered in relation to material flow and mold release.
Areas where air can become trapped should be identified during mold development.
The trimming strategy should be considered from the beginning because the forming boundary and final product boundary are not always identical.
A stable process is normally developed step by step rather than by changing several parameters simultaneously.
A practical development sequence is:
Review:
Confirm:
Review:
Determine:
The objective is to establish a suitable thermal condition before forming.
Evaluate:
Inspect:
Adjust one major variable at a time where possible.
This makes it easier to identify the actual cause of a process change and establish repeatable production conditions.
For complex thick-sheet parts, the final result is determined by the interaction of multiple variables.
A simplified relationship is:
Material + Sheet Thickness + Heating + Mold Geometry + Vacuum + Forming + Cooling = Final Part
Changing one variable can affect several others.
For example, increasing heating intensity may improve forming depth but can also increase localized stretching.
Increasing vacuum performance may improve mold replication but may also reveal weaknesses in material distribution.
Changing mold radius may improve material flow while changing the final dimensional behavior of the part.
This is why successful heavy gauge thermoforming requires the process to be developed as a complete system rather than optimizing individual machine settings independently.
There is no single universal thickness boundary used across all industries. The term “heavy gauge” generally refers to thermoforming applications using substantially thicker sheet than conventional thin-gauge packaging applications. The appropriate process depends on the material, part geometry, and production requirements rather than thickness alone.
Thicker sheet takes longer for heat to penetrate through the material. The surface can reach the desired temperature while the core remains cooler, creating a temperature gradient that affects forming behavior and material distribution.
Not necessarily. Forming stretches the sheet, and different areas may experience different amounts of deformation. A thick starting sheet can still develop localized thin areas around deep features, corners, or other regions with high material movement.
The mold determines how the heated sheet moves and stretches. Deep cavities, sharp transitions, small radii, and other geometric features can concentrate deformation in specific areas.
Vacuum forming depends on removing air between the sheet and mold. If air cannot escape efficiently, the sheet may fail to contact certain areas of the mold, resulting in incomplete forming or poor surface replication.
Yes. Complex parts can be thermoformed when the material, heating profile, mold geometry, forming method, vacuum distribution, and cooling conditions are properly matched to the part requirements.
Warpage can result from uneven cooling, residual stress, uneven wall thickness, material shrinkage, mold temperature differences, or removing the part before it has developed sufficient dimensional stability.
Process optimization normally involves evaluating the material, sheet thickness, heating profile, mold geometry, vacuum performance, forming sequence, cooling conditions, and final part dimensions together. Controlled trials are used to establish a stable process window.
Heavy gauge forming is closely connected with several other areas of thermoforming engineering:
Heavy gauge thermoforming is not simply a matter of heating a thick plastic sheet and applying vacuum.
The quality of the finished part depends on how heat moves through the sheet, how the material redistributes during forming, how the mold controls that movement, how air is removed, and how the part is cooled and stabilized.
For demanding applications, the forming process should therefore be developed from the part geometry backward:
Part Requirements → Material → Sheet Thickness → Mold Geometry → Heating → Forming → Vacuum → Cooling → Final Inspection
This engineering approach provides a more reliable foundation for developing repeatable heavy gauge thermoformed parts.